In a cooking oil producer’s logistics process, safely and efficiently transporting finished oil from the workshop to the warehouse or loading area is a common challenge. Barrel-packed cooking oil is heavy and prone to rolling, creating a falling risk during conveyance. By deploying Naili Conveyor’s multi-wedge belt powered roller conveyor and innovatively adding protective rails on both sides, the company successfully solved the issue and achieved safe, continuous internal workshop transport.
Case background and demand analysis
There is a distance between the cooking oil company’s workshop and finished goods warehouse, and previously barrels were mostly moved manually or transferred by forklifts. This method was labor-intensive, inefficient, and frequent handling increased the chance of dents or accidents. The company wanted a conveyor system to automatically connect the end of the production line with the warehouse while ensuring absolute safety, preventing barrels from falling off the conveyor.
Solution: multi-wedge belt powered roller conveyor with added protective rails
To meet the customer’s requirements, Naili Conveyor recommended the multi-wedge belt powered roller conveyor as the core equipment. It uses motor drive, synchronizing all rollers through the multi-wedge belt to deliver steady, continuous power for barrel transport.

To completely eliminate the risk of goods falling, we installed detachable metal safety rails along both sides of the conveyor. The rail height was carefully designed to block barrels from rolling out without obstructing workers’ necessary operations and visibility. This combination of powered conveyance plus physical protection perfectly meets the customer’s dual needs for efficiency and safety.
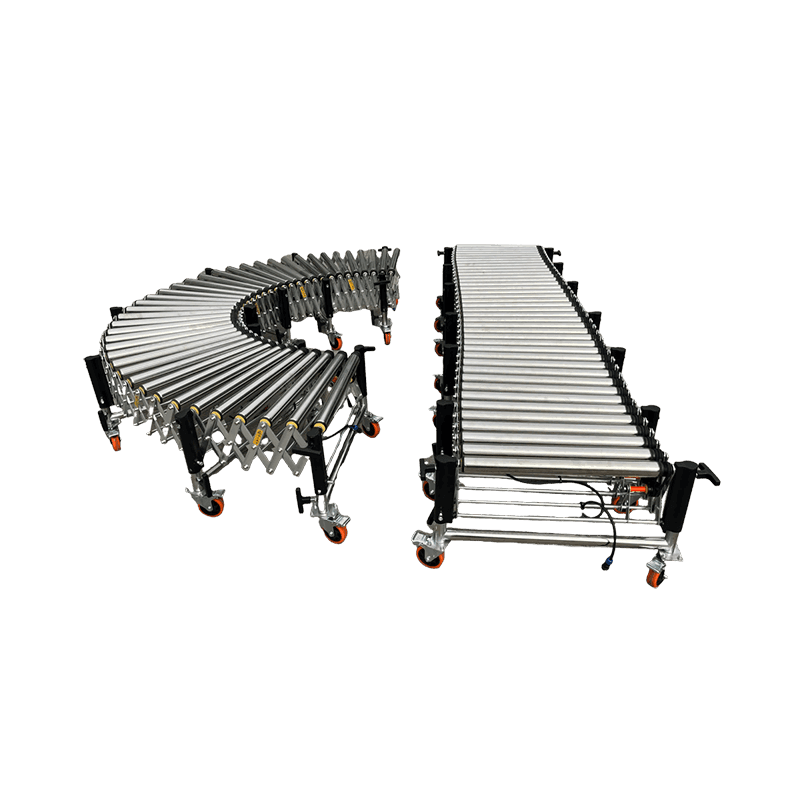
Transportador de rodillos accionado por correa de múltiples cuñas
The multi-wedge belt Powered Roller Conveyor uses a multi-wedge belt drive design to achieve smooth and efficient cargo conveying. Motor spacing range...
 Bidón de plástico
 Bidón metálico
 Caja de cartón
 Rodar
Solution implementation and results
The line was custom-designed and installed according to the workshop layout, seamlessly linking the production line discharge point with the warehouse intake area. Once the system starts, barrels from the production line are placed at the conveyor start and automatically move forward under the driven rollers. The side rails act as a "safety corridor, " guiding the barrels steadily along the predetermined path until they reach the warehouse end for stacking or further handling.
After implementing the solution, the results were evident:
- Enhanced safety: The side rails thoroughly eliminate the risk of barrel falls during transport, protecting both goods and personnel.
- Improved loading efficiency: Achieved continuous transport from production to warehousing, reducing intermediate handling and greatly boosting logistics turnover.
- Reduced labor burden: Workers only need to load at the start and organize at the end, avoiding heavy mid-transfer work and significantly lowering labor intensity.
Solution advantages and applicable scenarios
The railing-equipped multi-wedge belt powered roller conveyor used in this case demonstrates its outstanding advantages in specific scenarios:
- Targeted protection: Provides an effective safety solution for transporting easily rolling cylindrical goods (such as oil drums, gas cylinders, paper rolls).
- Flexible configuration: The rails can be partially or fully installed as needed and designed as fixed or quick-detachable to suit different operational demands.
- Reliable power: The multi-wedge belt drive runs smoothly, quietly, with simple maintenance, ideal for workshops requiring long-duration continuous operation.
This solution is not only suitable for liquid packaging industries like cooking oil and lubricant oil but also for workshops in chemical, food, paper, and other sectors that need to transport barrel, tank, or roll goods internally.
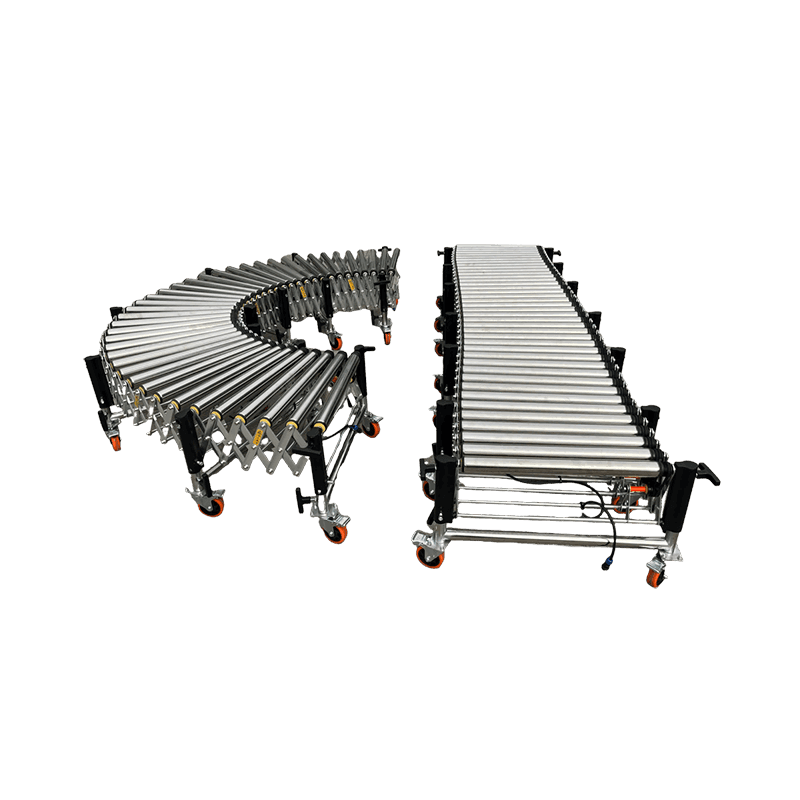
Serie de transportadores de rodillos motorizados
The powered roller conveyor is designed specifically to meet conveying needs for the final stretch of loading and unloading, enabling continuous and s...
Bidón de plástico
Bidón metálico
Caja de cartón
Rodar
Conclusion
By adding side rails to the multi-wedge belt powered roller conveyor, Naili Conveyor created a safe and efficient internal transport lifeline for the cooking oil customer. This case proves that tailoring protective modifications to standard conveyors based on specific goods characteristics and risk points can significantly improve logistics safety and reliability at reasonable costs. It provides a practical reference solution for companies with similar transport protection needs.